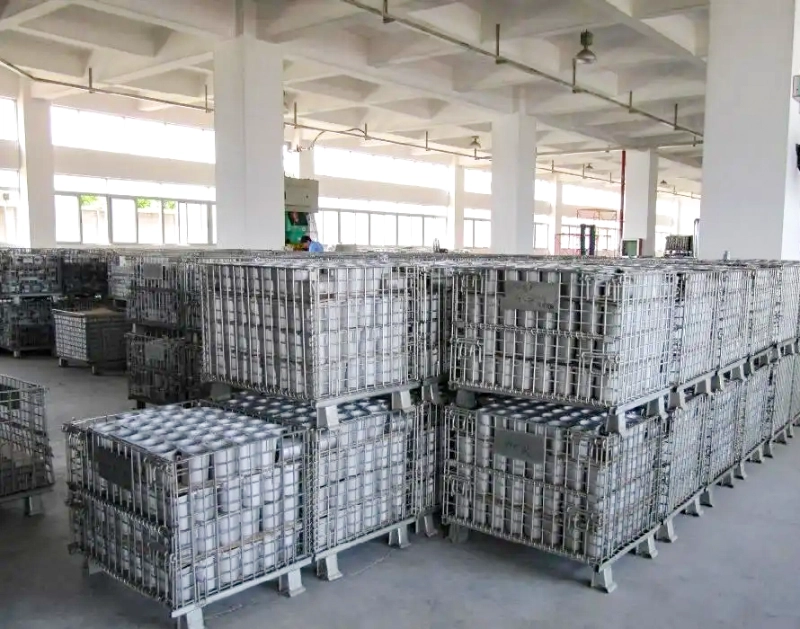
An inline buffer only earns its floor space when the operator can actually reach its contents. Stack the containers and fill them with castings, and the part the operator needs is usually in the cage at the bottom of the stack. That turns a short pick into a forklift call, an unstack, a dig through the top container, and a re-stack, with the line down the whole time. That unstacking, not the container price, is the cost that quietly eats an inline stock.
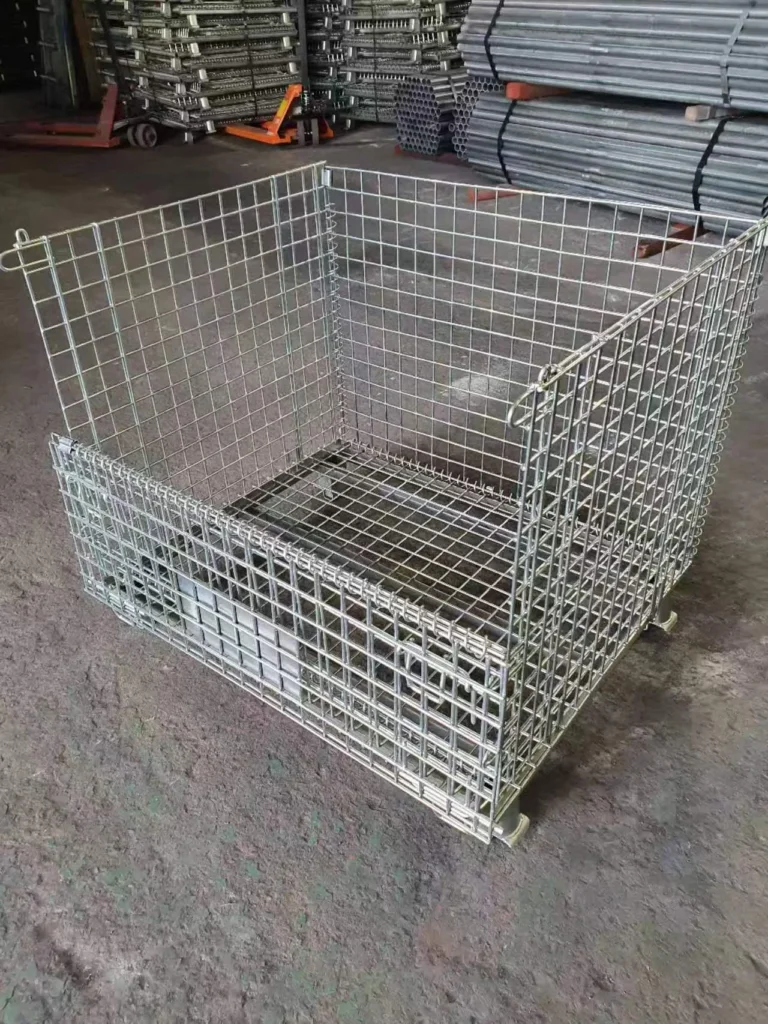
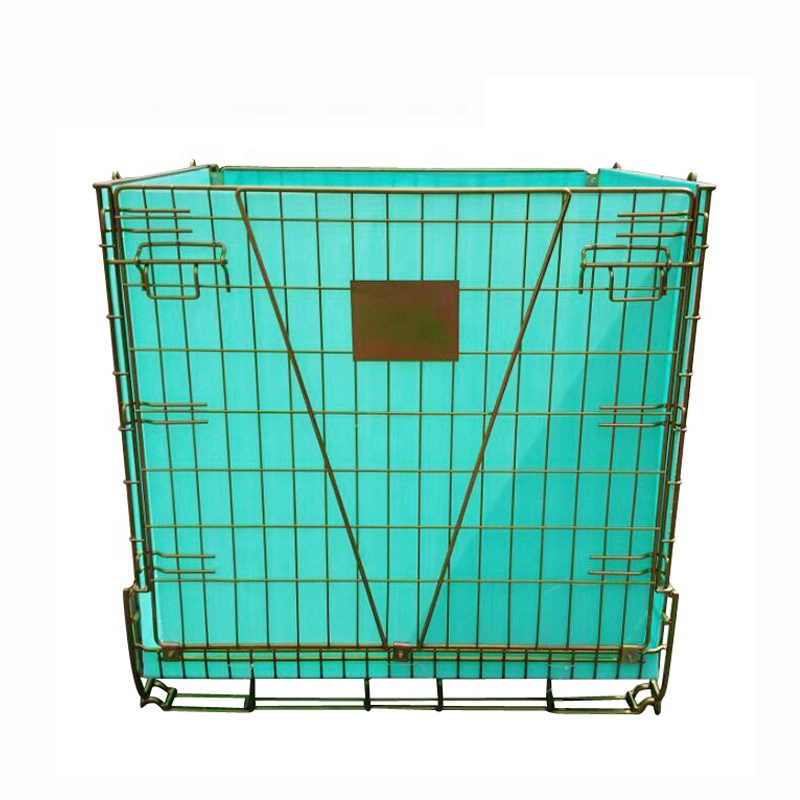
A drop-gate wire mesh container is designed around that single moment. One face of the container carries a half-drop gate: the upper half of the front mesh panel unlatches and folds down, so the operator picks parts from the container face at working height while the stack above stays seated. The same cage still folds flat when empty and takes forklift and pallet-truck handling, so the picking feature does not cost you the empty return trip. The following explains how the gate works in an inline flow, what the 50×50 mm mesh does and does not do for inventory visibility, when small parts need a liner, and how to orient the gate face to the aisle.
How does a half-drop gate let you pick without unstacking?
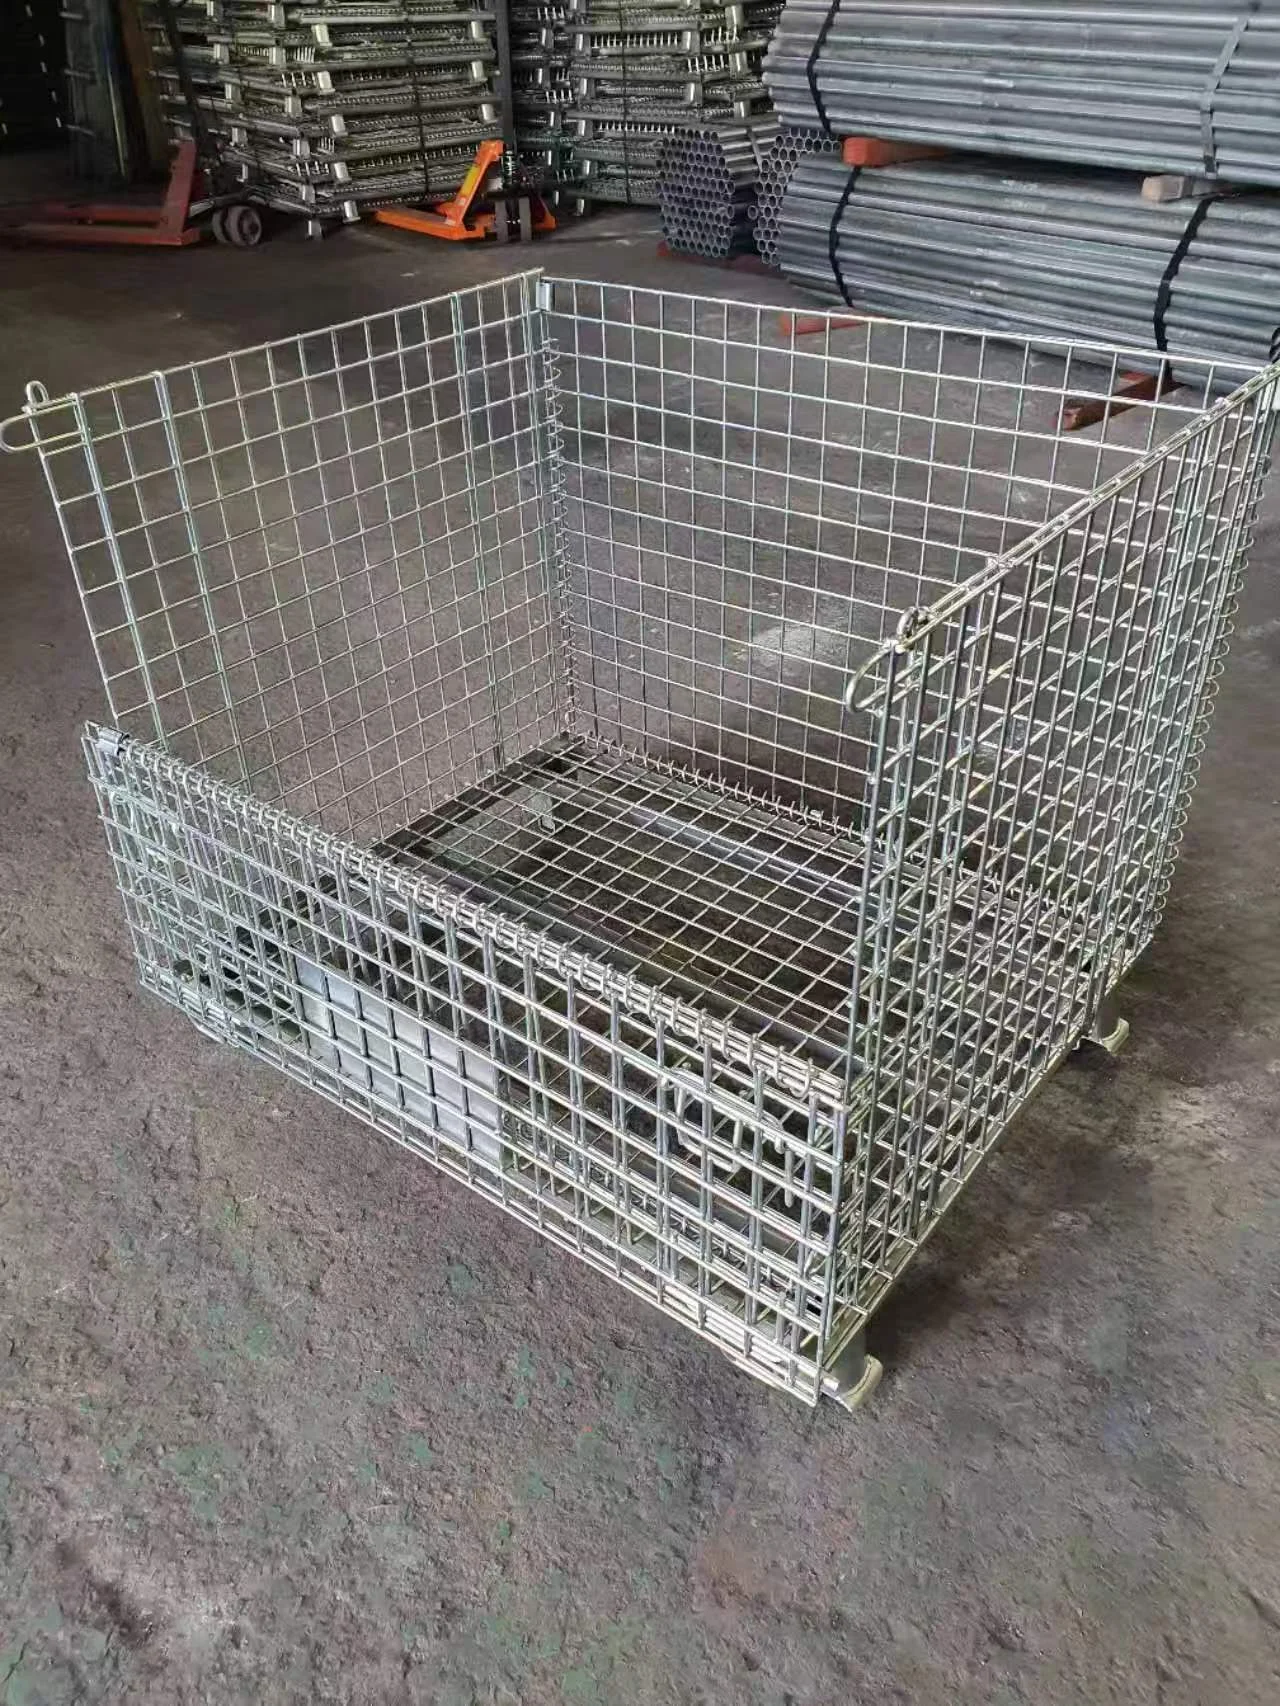
In the documented configuration, the half-drop gate is a single-face feature. The upper half of the front panel is carried on a piano-hinge line, unlatches, and folds down roughly 180° to lie against the outside of the lower panel. The lower half of the panel, the base frame, and the formed stacking feet stay as they were. That matters more than it sounds: a stack's load travels down through the feet into the base channels, so folding only the upper panel leaves the seat under the container above intact. The operator reaches over the dropped panel and takes the part, with no forklift, no unstack, and no re-stack.
The floor-level picking sequence
- Walk up to the gate face; nothing above or below the container has to move.
- Release the latch pins on the upper panel.
- Fold the upper panel down until it rests against the lower panel.
- Pick the part from the exposed face; the lower panel still retains the remaining parts.
- Fold the panel back up, re-latch it, and confirm the face is closed before moving or stacking the container.
Where the gate stops helping
The gate is a picking access, not a discharge door or a reach extender. If the part you need is in a container stacked above your reach height, the panel still opens, but your arm does not get longer, so that level needs a platform, a step, or a hoist. If picking is a full-container dump, where the whole contents go to the line at once, a half-drop gate adds a step to a job that a simple open container or a tilt frame handles faster. And if the container is going to be tipped or machine-dumped, the gate must be closed before the lift: an unlatched panel under a tipped load is an accident waiting to happen.
Does the 50×50 mm mesh give you a reliable count?
The mesh on the recorded projects is a 50×50 mm welded steel wire grid, and it is the reason an operator can see into a closed container. Through the side panel or the open gate you can read fill level, spot a nearly empty container before the line stalls on it, and confirm the buffer holds the part numbers it should. All of that happens without opening a lid, unlatching a panel, or lifting a cage off a stack.
That is visual control, and it is genuinely useful between counts. It is not a count. Deep stacking hides every layer under the top one; small identical parts loose in bulk cannot be counted through a grid, however good the light; and a mixed-part container defeats visual verification entirely. The inline operating rule is to use the view through the mesh as a between-counts check, keep one part number per container, keep a label or kanban card on the gate face at eye level, and still run the cycle count on its own schedule. Visual control reduces how often you have to open, dig, and recount a container. It does not eliminate counting, and no mesh opening can promise zero inventory errors.
Will small parts fall through the mesh?
The mesh is a hole with a frame around it. A 50×50 mm opening retains most industrial components and lets anything smaller than the opening through: out the side panel during handling, out the gate when it is folded, or onto the floor when the container is moved on a pallet truck. So the check is the smallest dimension of the smallest unit part you intend to store, not the average part or the package size.
If that dimension can pass through the opening, the plain mesh container is the wrong container for that part. The options are a PP hollow-sheet liner that turns the cage into a five-sided barrier, a mesh specification with smaller openings budgeted as a variant, or a solid-walled container. Two consequences are easy to overlook. A liner blocks the view through the mesh, so a lined cage loses visual counting on the lined faces. And long, thin parts can protrude through the open gate, so measure the gate swing area and keep it clear of aisles and truck routes. If parts can bounce or be thrown out through the open top, a closeable-lid variant closes the container.
Which way should the gate face?
Gate orientation is a layout decision, and it is far cheaper to settle before the order than after the first delivery. Four things to fix on the floor plan:
- Picking side: the gate faces the operator's walking route, never a powered pallet truck lane. A panel that folds into pallet truck traffic is a collision, not a feature.
- Handling side: the registered base accepts forklift and pallet truck entry from four sides, so the pallet truck can approach from any face, which leaves the gate side free to be chosen for the picker rather than the pallet truck.
- Height: arrange the buffer so that the containers whose gates are used for picking are the ones within reach. A two-high stack with the gate on the lower container at picking height is the simplest arrangement; the upper container is stock, not a picking face.
- Movement: if the buffer moves by pallet truck between stations, the gate comes back on a different side each time. Either mark the container orientation on the floor plan so the gate returns to the same side, or use a wheeled-base variant and turn the gate toward the station with the brakes set.
Configuration options and when each one fits. The variants below follow the documented configuration set and the indexed images; confirm the variant list on the drawing before ordering.
| Configuración | What it solves | When it is not the answer |
|---|---|---|
| Half-drop gate on one face, fixed base | Picking from a stacked container without unstacking | Full container discharge, or parts stored above reach height |
| Half-drop gate with PP hollow-sheet liner | Small or precision parts that would pass through or rub against the mesh | Where the fill level has to remain readable through the mesh |
| Half-drop gate with wheeled base | A buffer that has to travel to the station | Routes where a rolling load is not under control |
| Closeable-lid variant | Parts that can bounce, or that need security | Frequent top loading, where the adds a handling step |
| Plain mesh container, no gate | Containment where picks only happen at unstacking | Any in-line flow where a pick must not wait for a pallet truck |
Where a drop-gate container fits in an in-line warehouse
- Machining cell buffer: one part number per container, gate toward the operator's walking route, buffer sized for one shift.
- Assembly line warehouse: two-high stack, gate on the lower container at picking height, upper container kept as stock.
- Mixed-model changeover: label the gate face and keep the container unlined whenever the fill level has to remain readable.
- Precision and electronic components: lined container with lid where the smallest part sits below the mesh opening.
- Mobile buffer: wheeled base so the gate can be presented to the station, brakes set before picking.
- Not for: full container discharge, loose parts smaller than the mesh opening without a liner, and parts whose length exceeds the swing area of the open gate.
Frequently asked questions
How much picking time does a half-drop gate really save?
It removes steps, not a fixed number of seconds: the pallet truck call, the unstacking, the search and the re-stacking disappear for parts stored in a container the operator can reach. What that is worth depends on your picking frequency, your stacking height and how often the wanted part is in the lower container. Measure those three and the saving follows from your own cycle data; we do not publish a percentage that was not measured in your layout.
Can we stop counting and rely on the view through the mesh?
No. The mesh provides a fill-level and presence check between counts. Deep stacking, small bulk parts and mixed part numbers break that check, so cycle counting stays on its own schedule and the visual view remains the quick check in between.
Can the container be moved or stacked with the gate folded down?
No. Fold the panel back and re-latch it before lifting or stacking the container, and confirm the latch before the unit leaves the picking position.
If the in-line buffer is where you are losing your takt, send the parts list, the smallest part dimension, the stacking height you handle and the minimum aisle length. We will confirm the gate face, the container size and the liner decision against the drawing before you order, and the empty return trip of the same container is covered in the companion article on folding.
¿Necesita una Solución de Almacenamiento a Medida?
Hable directamente con nuestros ingenieros técnicos. Ofrecemos diseños estructurales gratuitos, evaluaciones de catálogos para cargas pesadas y cotizaciones de precios B2B rápidas.
Solicitar un Presupuesto Ahora →