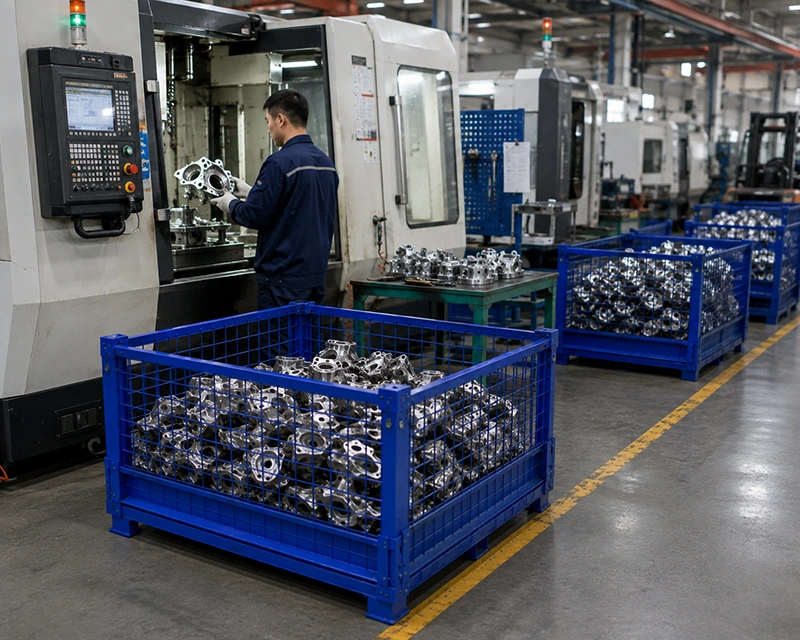
Between two assembly stations the distance is often short and the cost is not. Loose castings, machined housings and pressed brackets leave one station in a bin or on an open pallet, are counted, carried, set down, waited for, and then lifted part by part into the next setup. Each of those steps is a handling operation that swallows labor time and creates the chance that a part falls, gets mixed with another batch, or is damaged against the floor.
The alternative is to stop treating transfer as a loose-materials problem. A collapsible cage pallet changes the unit of work: the batch leaves a station already in a rigid, pallet-shaped, stackable steel container that a forklift or pallet truck moves in one motion, and the next station takes the parts out without unpacking. This article describes how that closed loop between stations is designed, what it costs to keep doing it manually, and under what circumstances a cage pallet is the wrong container for the job.
Why transfer between stations needs a fixed unit, and not just a container that happens to be nearby
Assembly line logistics relies on repeatable geometry. Aisle width, line footprint, forklift fork spacing, rack beam level and turning circle at the dock are all planned around one standard load volume. A loose bin that changes size every shift breaks that planning: the same batch can have a different footprint on Monday than on Wednesday, and a stack of mismatched containers cannot be planned at all. A cage pallet fixes four things at once — outside dimensions, internal working height, base entry and own weight. That gives the line engineer something to design on: one position on the floor per load, one fork entry per move, one empty footprint when the container is collapsed.
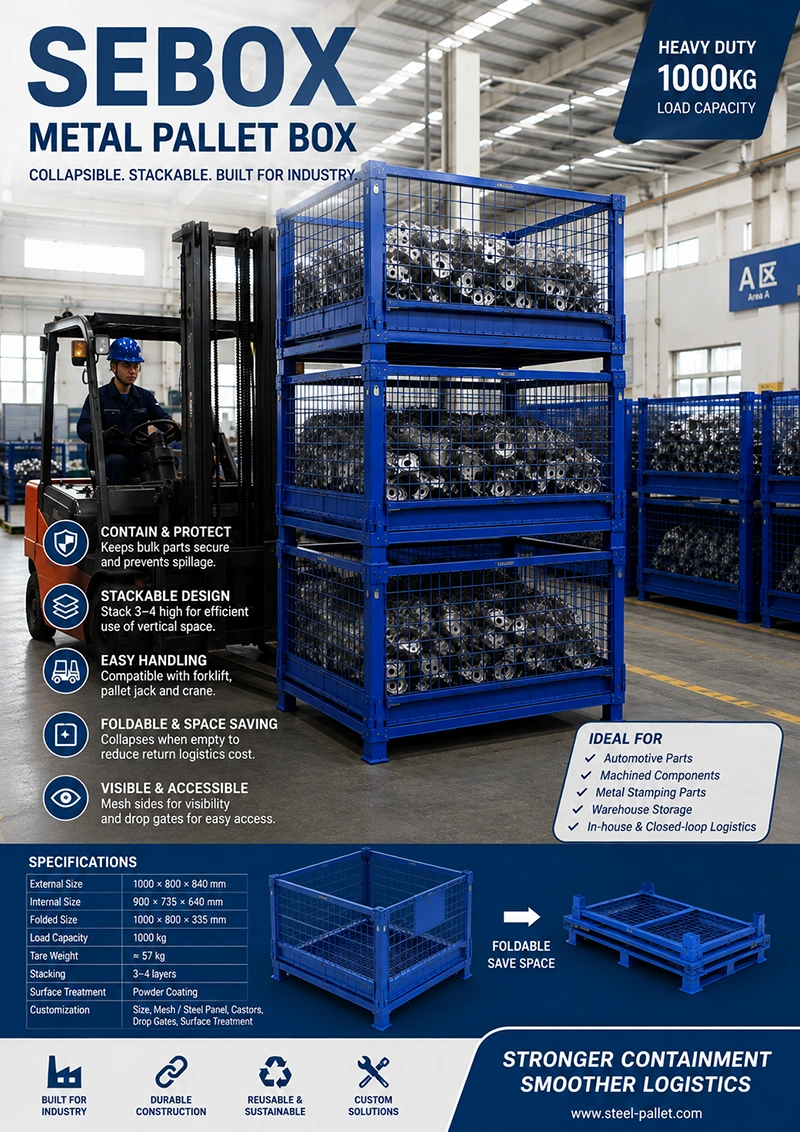
The load capacity on a product image is not a series-wide value. The Sebox family is documented with at least three different variants — one with a design load of 1000 kg and a collapsed height of 335 mm, one with 1300 kg uniformly distributed, and one with 1500 kg uniformly distributed, on different outside dimensions and weights. Which figure applies to your line is recorded on the approved drawing for that SKU, together with the base plate thickness, the tube profile and the panel type.
Where the costs of manual handling actually pile up
Manual transfer is rarely one big cost item. It is a chain of small ones, and that chain repeats once per batch per shift. A typical transfer of loose parts between a machining cell and an assembly bench includes the following operations: pick parts from the machine outlet; place in a bin; stack or carry the bin; set down at the station; wait for a free operator; lift parts out and place in the setup; return the empty bin. Six or seven touches, each with its own risk of a dropped part, a mixed batch and a reach-and-bend injury, and each with an operator minute that adds nothing to the product.
Bundling the batch per unit reduces the chain to a mechanical move plus a pick. The container is loaded once at the supply side, moved as one load with a forklift or pallet truck, and placed at working height at the next station. The operator touches the part twice — once in the container, once out — instead of six times. Nothing in that calculation is a fixed savings percentage; the real figure depends on your batch size, your station distance and your current bin handling, and that is why the change must first be measured on one loop before it is rolled out across the whole factory.
Visual stock is what keeps the line from stopping
Line stoppage usually starts as a surprise: the station ran dry because no one saw it coming, because the batch was at the back of a stack in a closed bin, or because the part could not be counted without unloading. Mesh sides tackle the visibility problem directly — a supervisor walking down the aisle can read fill level, part shape and batch composition through the panel, and a nearly empty container is visible before it becomes an andon call. That is the practical reason assembly plants put mesh and not sheet steel on the line side.
There are limits to visibility that must be stated up front. Mesh lets you see a large, uniform part; it does not let you count a heap of small loose pieces through the panel, and it does not keep out chips, dust or coolant mist. It also does not help if the container is buried in the third layer of a stack — and that is why the front gate matters as much as the panel. A half-drop front gate, documented on various Sebox versions, allows an operator to unlock the upper half of the front panel, hinge it down, pick the part and close it again while the container stays in the stack. Used together — mesh to see, gate to reach — the station can be replenished and picked without breaking down the stack for access.
Making the mechanical loop work: base entry, mobility and the empty return
A closed loop has three states: loaded, empty and in transit. The base determines the first two. Sebox bases are documented with forklift-compatible feet and recesses, with four-sided access on some configurations, so the container can be approached from the aisle where it actually stands rather than a theoretical one. Where the loop is short and flat, swivel castors and a drawbar appear in documented and pictured configurations, turning the container into a mobile unit that an operator can push from the cell to the bench without a truck; that option must be specified per SKU, because both the castor load capacity and the floor condition affect it.
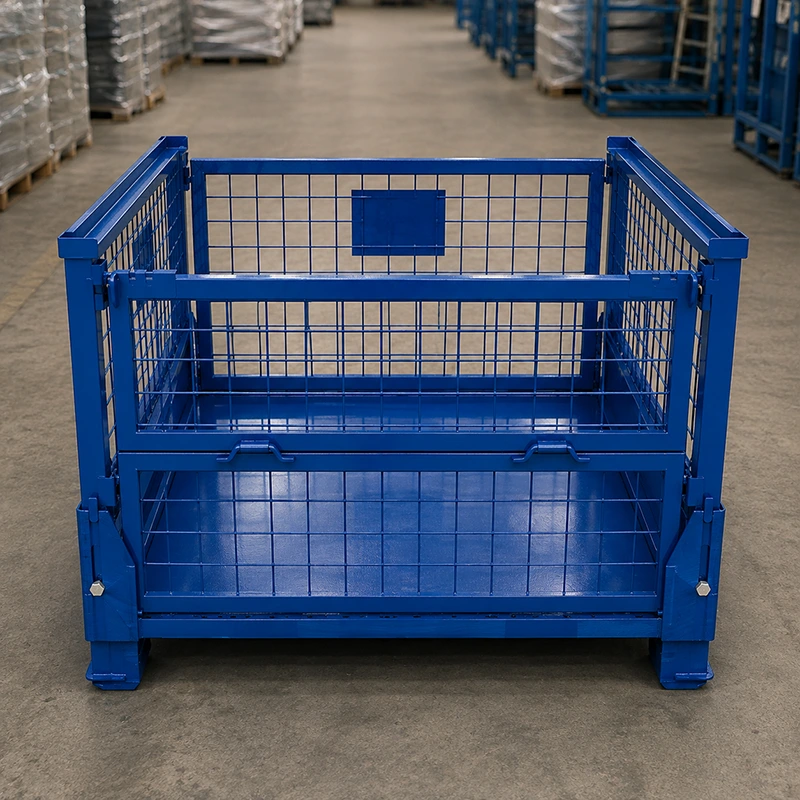
The empty state is where a rigid steel container loses money if it is poorly designed. Collapsibility addresses this: the documented Variant C collapses to a 1000 × 800 × 335 mm profile from an 840 mm working height, and the 1220 × 1015 mm variant also collapses to 335 mm. Those are variant-specific figures, not a family-wide rule, but the principle holds across the range — an empty bin that stacks flat returns in a fraction of the cube it occupied when loaded, and that is what makes a closed loop between stations cheaper than a one-way packaging flow.
Conditions where a cage pallet is not the right choice
A cage pallet is a containment device for parts that return, and should be refused where that is not the case. The following conditions require a different specification or a different product, and should be clarified before any quotation:
- Parts smaller than the mesh size, or parts that produce fine swarf: mesh alone lets material escape. Instead of a full mesh container, specify solid steel panels, a liner, or a mixed base-and-gate version.
- A one-way export route without a return loop: if the container does not come back, folding and reusability achieve nothing, and single-use packaging per shipment is likely cheaper.
- Stacking claims beyond the drawing: documented sources give a recommendation of 3–4 layers for one variant and a maximum stacking height of 5 m for another. Both are configuration- and location-dependent, so the layer count, the permitted total load on the bottom container and the floor or rack condition must be confirmed for your SKU.
- Load assumptions from a photo: a figure on a poster such as 1000 kg belongs to the variant it was printed for. Uniformly distributed load and impact load from a dropped casting are different cases and are not interchangeable.
- Corrosive, wet or exposed application: the standard finish is a powder or spray coating, with galvanised and stainless steel options listed in the customisation table but not linked to every variant. Outdoor use or washing requires that link to be confirmed.
- Certification-driven purchasing: Gitterbox is a strong European search term and a useful benchmark reference, but here it is a descriptive term, not a proven certificate of conformity. Buyers who need formal conformity documentation should include this as an explicit requirement rather than inferring it from the product name.
What to include in the line-side requirement
A supplier cannot dimension a cage pallet loop on the basis of the sentence "we need some cages". The loop is defined by your data. Send the parts list with weights and the largest dimension, the batch quantity per station per shift, the working height of the pick face on both sides, the forklift or pallet truck you intend to use and the fork spacing, the available line-side area including the access aisle, the number of layers you want to stack and what sits above the bottom container, the route of the empty return and the vehicle, and the finish or washing requirement. With this data the container can be configured — panel type per side, gate version, base access, castor specification and collapsed shipping dimensions — and the load figure can be recorded on a drawing that the line engineer signs off.
To take the next step, view the interstation transfer scheme for collapsible cage pallets, or send your line-side requirement with the parts list and station layout so the loop can be quoted on the basis of your own figures rather than a catalogue average.
Where this configuration fits
- Machining cells and CNC workshops that route batches of finished parts to a downstream assembly bench.
- Automotive sub-assembly lines where castings and pressed parts must arrive at the fixture in a known quantity and orientation.
- Work-in-process buffering between processes, with optional swivel castors where the movement is short and the floor is flat.
- Plants that need the same container line-side, in warehouse block stacking and in an overseas container on the return.
Veelgestelde vragen
Can one cage pallet design serve every station on the line?
Only if the part envelope and the batch quantity are genuinely comparable. One footprint simplifies forklift and layout planning, but the load rating, the panel type and the gate version must still be valid for the heaviest part per station. Where one cell runs large castings and the next runs small fittings, two configurations from the same family are usually cheaper than forcing one oversized container through both.
Do I need a half-drop gate on every side?
Nee. Toegang is nodig waar het picken plaatsvindt, wat in de meeste indelingen één kant is die naar het gangpad of naar de positie van de operator wijst. Alle kanten van een poort voorzien voegt kosten en hardware toe zonder de doorvoer te verhogen. De uitzondering is een container die tijdens de loop wordt geroteerd, in welk geval het specificeren van twee tegenover elkaar liggende poortkanten de moeite waard is.
Hoe bepaal ik de stapelhoogte voordat ik koop?
Request the approved drawing for your exact SKU and check three numbers together: the allowable load in a single container, the allowable total load resting on the bottom container, and the maximum stack height permitted for the floor or rack condition at your site. Published family recommendations differ because the variants differ; the drawing is the only document that binds the answer to your container.
Heeft u een op maat gemaakte opslagoplossing nodig?
Spreek rechtstreeks met onze technische ingenieurs. Wij bieden gratis constructieontwerpen, evaluaties van zwaar belaste catalogi en snelle B2B-prijsopgaven.
Vraag nu een offerte aan →